 xrguo@xinhaimining.net
 +8618733132385
 +8618733132385


Antimony Ore Beneficiation Equipment and Optimized Processing Flow
2026-08-31 Xinhai (54)
2026-08-31 Xinhai (54)
If you have any questions, please contact us through the following ways, we will give you more and better assistance!
Antimony is an indispensable strategic mineral widely used in flame retardants, alloy manufacturing, chemical engineering and military industries. Natural antimony ore mainly consists of stibnite and antimony oxide, often symbiotically associated with quartz, calcite, pyrite and other gangue minerals. Most raw antimony ores feature uneven grain size and complex intergrowth, making professional beneficiation equipment and targeted process design essential for improving concentrate grade and resource recovery rate. Modern antimony processing adopts a mature combined gravity-flotation flow, delivering high efficiency, low energy consumption and stable production performance.
Complete antimony beneficiation production lines cover crushing, grinding, desliming, separation and dewatering systems, with each stage equipped with dedicated professional equipment to adapt to different ore properties.
Crushing and closed-circuit grinding serve as the foundation of efficient separation. Bulk raw ore is firstly processed by jaw crushers for coarse crushing and cone crushers for fine crushing to obtain uniform particle size feed. The matched ball mill and hydrocyclone group form a closed grinding system, which fully dissociates monomer antimony minerals from gangue impurities. This precise particle size control avoids over-grinding slime pollution and guarantees stable feeding conditions for subsequent separation.
Gravity separation equipment is the core pre-selection unit for antimony ore. Benefiting from the obvious density difference between antimony minerals and waste rock, sawtooth wave jigs and 6-S shaking tables are widely applied. Jig separators handle coarse and medium-grained antimony ore with large processing capacity and zero chemical consumption, efficiently extracting qualified rough concentrate and discarding most tailings. Shaking tables further refine fine-grained materials, effectively improving pre-selection recovery rate and reducing the load of subsequent flotation operations.
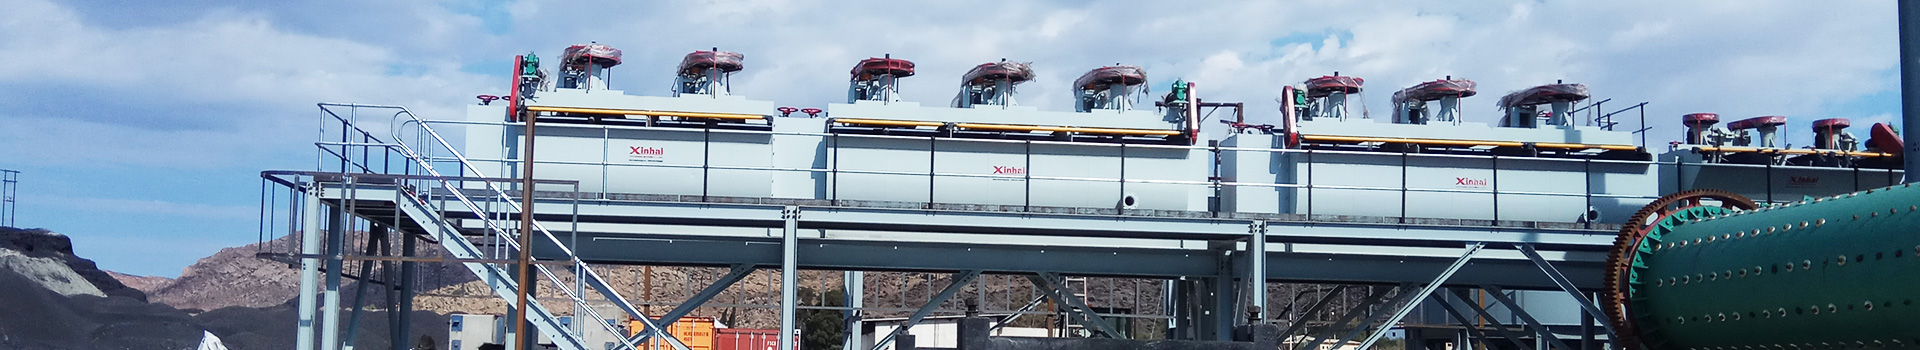
Flotation equipment is the key to high-grade antimony concentrate production, suitable for fine-grained and refractory antimony ore. Mechanical agitation flotation cells adopt a standard technological flow of one roughing, multiple cleanings and two scavengings. With selective collectors and inhibitors, the system effectively separates antimony minerals from pyrite and silicate impurities, stably upgrading the antimony concentrate grade. For low-grade and complex symbiotic ores, optimized flotation reagent systems significantly reduce metal loss and improve overall beneficiation indicators.
Supporting dewatering and auxiliary equipment ensures standardized finished products and green production. After separation, antimony concentrate is sent to thickeners for concentration and filter presses for solid-liquid dehydration, lowering moisture content to meet industrial sales and smelting standards. All tailings and wastewater can be recycled after treatment, realizing energy-saving and environmentally friendly operation.
In summary, the combined gravity-flotation process with professional supporting equipment is the most reliable solution for modern antimony ore beneficiation. Customized equipment selection and process optimization according to actual ore characteristics can maximize economic benefits, making it widely applicable for global antimony mineral development projects.


 Consult
 Message
 Email
